Welcome to JiuJiang LANZO New Materials Technology Co., Ltd.

- Home
- Products
- About Us
- Customized Process
- Applications/Solution
- News
- Contact Us
Leave Your Message
Welcome to JiuJiang LANZO New Materials Technology Co., Ltd.
High-potency chemical additives engineered to stabilize complex blends, improve solid-liquid separation kinetics, and satisfy rigorous industrial chemical processing standards.
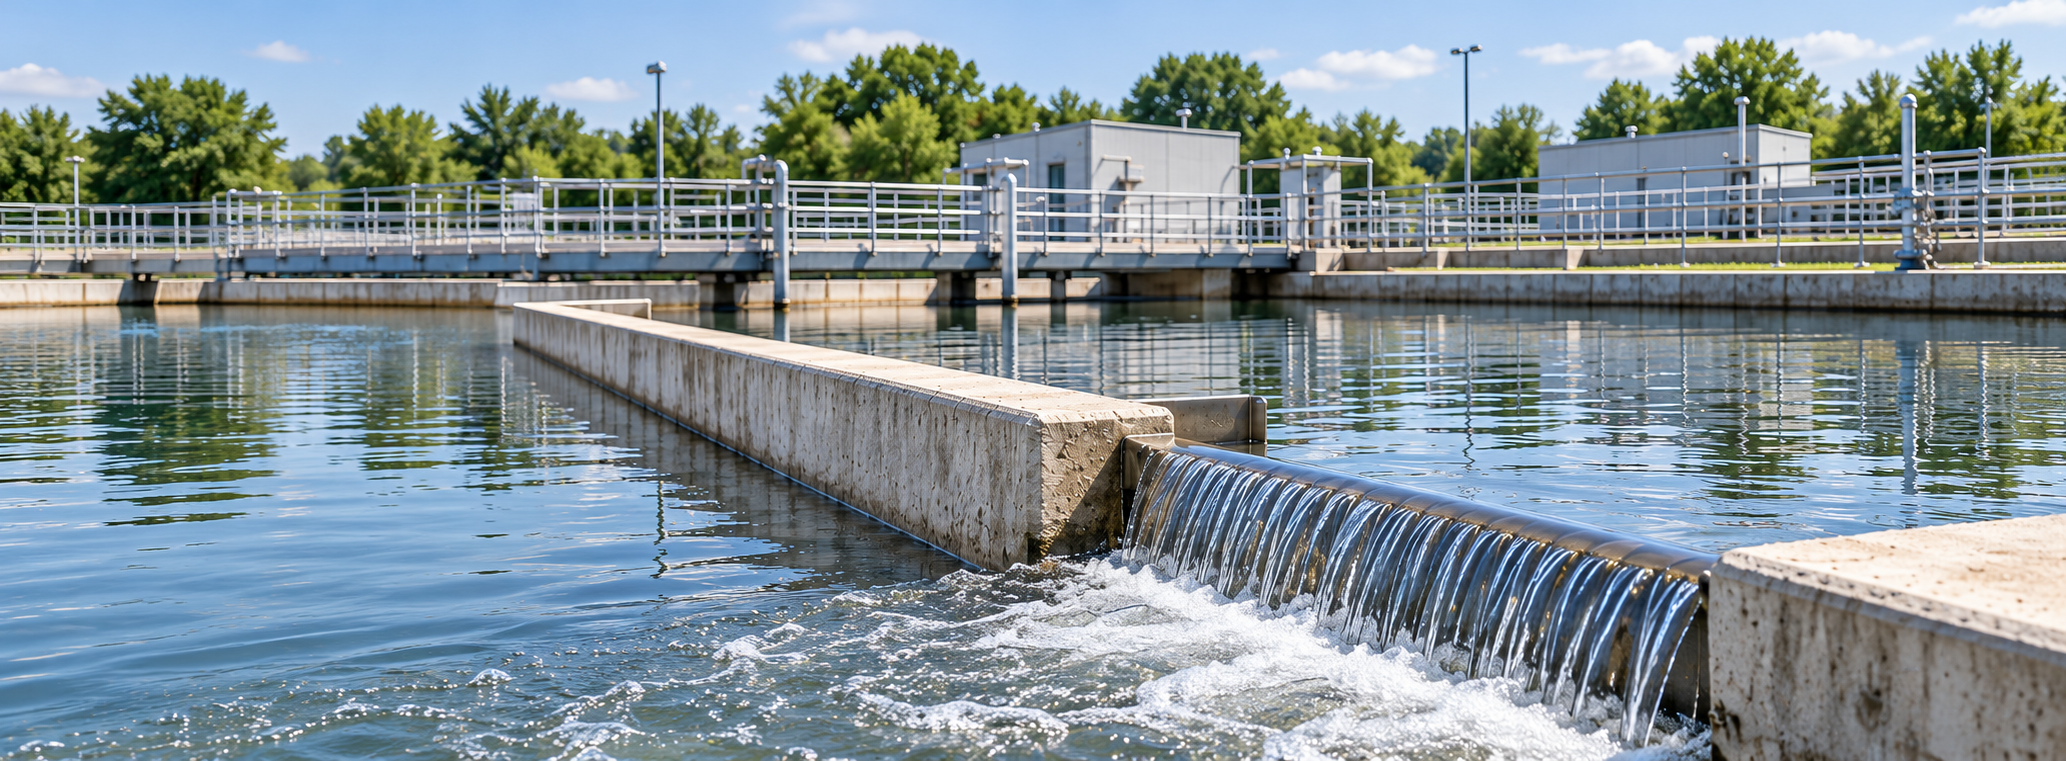
High-basicity inorganic-organic composite coagulants designed for high-turbidity water clarification and rapid micro-floc formation in chemical formulation plants.
Explore Formulation →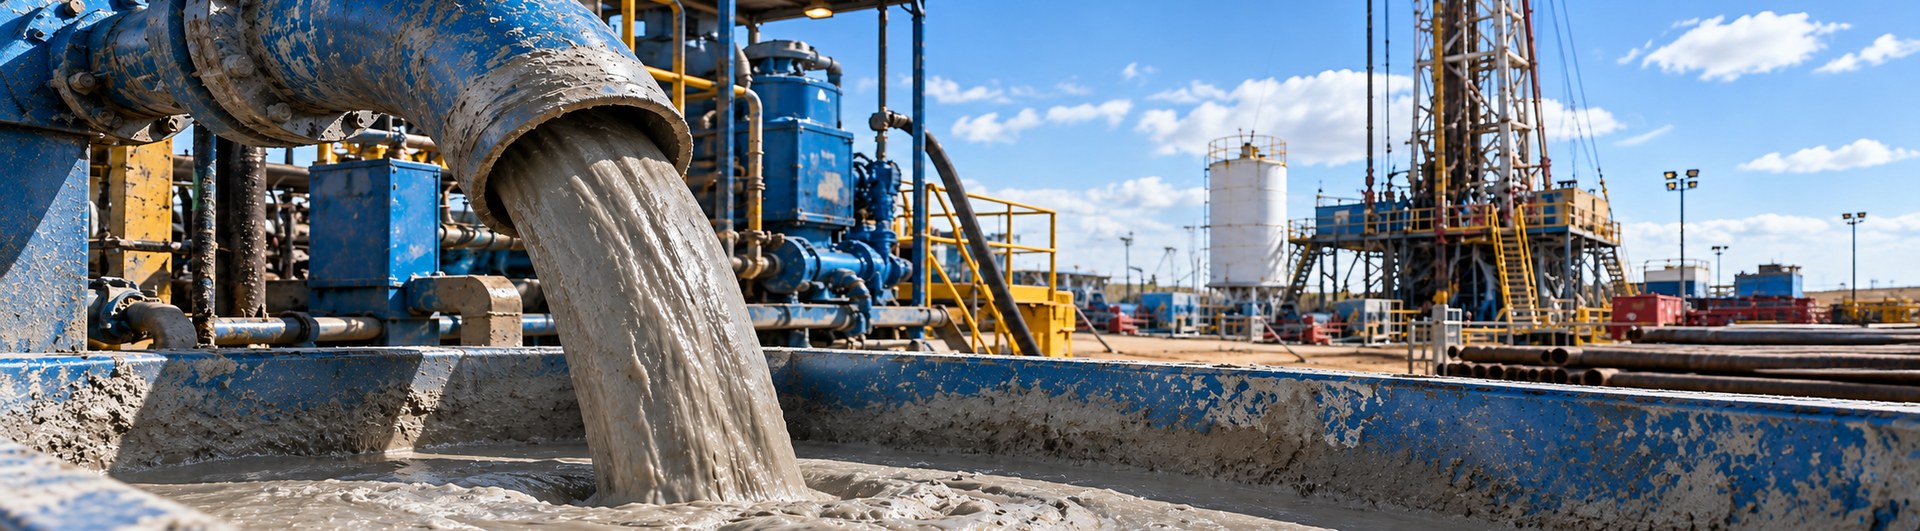
Polycarboxylate ether and sulfonate-based superplasticizers offering superior dispersion, viscosity thinning, and hydration control for chemical synthesis.
Explore Formulation →
Custom ionic-degree cationic and anionic polyacrylamide (CPAM/APAM) formulations tailored to optimize bridging affinity across industrial slurry filtration.
Explore Formulation →
Polyamine-based synergistic demulsifiers providing ultra-fast oil-water de-oiling, heavy metal chelation, and sludge density enhancement in petrochemical effluent streams.
Explore Formulation →Transforming complex chemical waste into recyclable process water via macromolecular design, smart coagulant dosing, and green chemistry synthesis.
In industrial chemical formulation, suspended colloids exhibit negative zeta potentials stabilizing colloidal suspensions. Modern cationic polymeric flocculants provide sharp electrical neutralization followed by extensive polymer bridging, destabilizing nanoparticles within milliseconds.
Modern chemical manufacturing facilities operate under stringent environmental discharge frameworks. Tailoring flocculants with high sheer resistance allows closed-loop water recovery loops, mitigating scaling, corrosion, and biological fouling across evaporators and crystallizers.
Lanzo leverages predictive polymer architecture synthesis, tuning molecular weights from 3 million to over 25 million Daltons and customizing charge density to eliminate chemical sludge volume by up to 35% compared to conventional alum or iron salts.
Petrochemical refining generates wastewater contaminated with emulsified aromatic hydrocarbons, naphthenic acids, and fine drilling mud particles. Standard coagulants frequently fail due to severe steric hindrance caused by synthetic surfactant packages. In custom industrial chemical formulation, our specialized amphoteric polyacrylamides and polydiallyldimethylammonium chloride (PolyDADMAC) complexes selectively displace oil-water interfacial films. This produces dense, shear-resilient flocs capable of rapid mechanical separation via dissolved air flotation (DAF) and decanter centrifugation, significantly reducing COD and total petroleum hydrocarbons (TPH).
In mineral extraction circuits—including copper, lithium brine, and rare-earth leaching—solid-liquid separation speed governs operational throughput. Custom water treatment flocculant formulations require targeted functionalization, such as hydroxamated polymers or ultra-high molecular weight anionic polyacrylamides. When dosed into dynamic thickeners, these formulations bind selectively to multi-valent mineral surfaces, expediting settling velocities to over 10 meters per hour and boosting underflow bed density for efficient paste backfill operations.
Specialty chemical manufacturers often discharge effluents containing up to 100,000 ppm total dissolved solids (TDS), making standard polyelectrolyte chains coil and lose flocculation performance. By incorporating salt-tolerant monomers like 2-acrylamido-2-methylpropane sulfonic acid (AMPS), our customized flocculant formulations maintain open hydrodynamic radius conformations in hyper-saline brines. This ensures uncompromised turbidity removal prior to reverse osmosis (RO) membrane desalination and high-pressure crystallization.
Mechanical dewatering costs constitute a dominant segment of waste handling expenses. The synergy between inorganic polyaluminum chloride (PAC) pre-conditioning and high-cationicity branched copolymers liberates trapped interstitial water within microbial and inorganic chemical sludges. Belt-press and filter-press trials demonstrate over 28% to 34% cake solids, driving down transportation logistics, incineration energy demand, and total carbon footprint.
JiuJiang LANZO New Materials Technology Co., Ltd. is a dynamic and innovative chemical enterprise established in 2019 and strategically located in Jiujiang City, Jiangxi Province, China – a region well-connected to major transportation networks for efficient global logistics. We specialize in the research, development, production, and sales of high-performance chemical additives, serving a diverse range of industries including oilfield exploration, water treatment, petrochemical refining, industrial manufacturing, and coatings production.
Our product portfolio encompasses oilfield chemical additives, water treatment agents, refining and fuel additives, industrial processing aids, coating auxiliaries, and advanced new materials. Beyond our standard offerings, we pride ourselves on our ability to deliver fully customized product development solutions, tailoring chemical formulations to meet the unique specifications and performance requirements of each individual client.
Our operations and business center is headquartered in Jiujiang, Jiangxi Province. From this strategic hub, we coordinate global supply chain management, order fulfillment, and technical support across our four core businesses—oilfield chemicals, water treatment, fuel, and industrial coatings. With convenient access to major transportation networks, we ensure efficient, reliable delivery to customers worldwide.
By synchronizing enterprise ERP with chemical distribution logistics, our operations ensure rapid response times, compliant hazardous material handling, and end-to-end batch traceability for our global partner network across Europe, Southeast Asia, the Middle East, and the Americas.
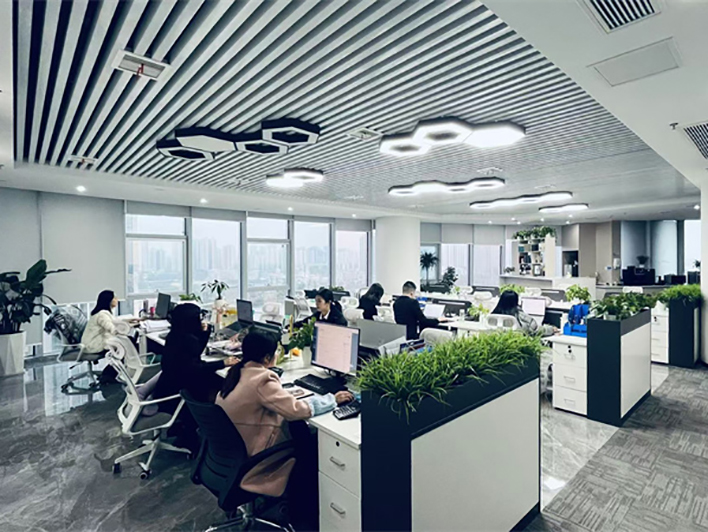
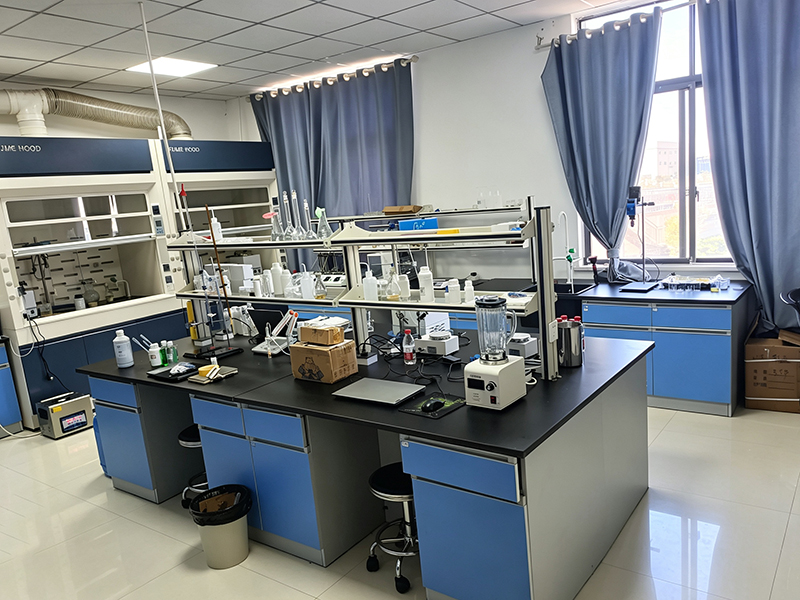
Our R&D and quality control laboratories are located in Jiangxi and Shandong provinces. Equipped with advanced testing instruments and staffed by experienced technical teams, our labs are capable of formulating and custom-developing products to meet diverse customer requirements. From raw material evaluation to finished product performance verification, every stage of laboratory testing and analysis is carried out with scientific rigor and precision.
Equipped with nuclear magnetic resonance spectrometers (NMR), gel permeation chromatography (GPC), high-precision laser particle analyzers, and high-pressure reactor arrays, our chemical researchers continuously innovate novel high-performance flocculation agents tailored to solve the most difficult wastewater clarification challenges.
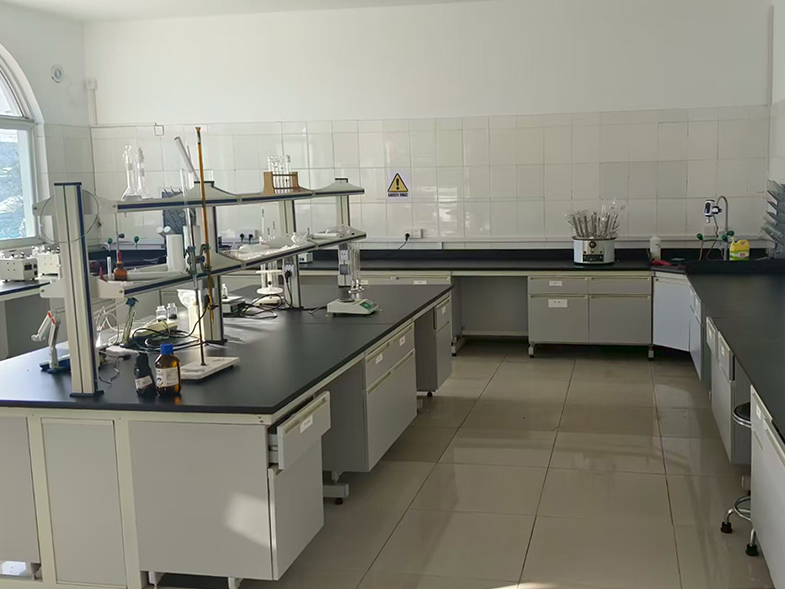
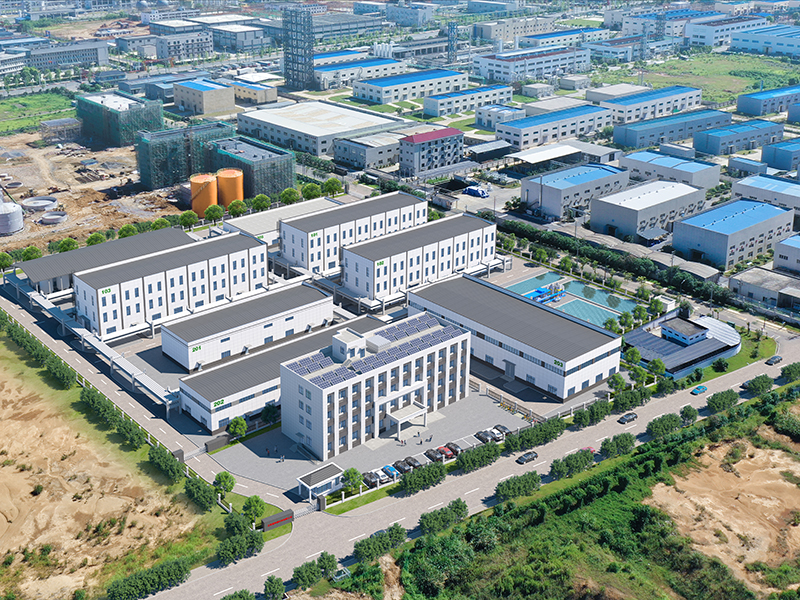
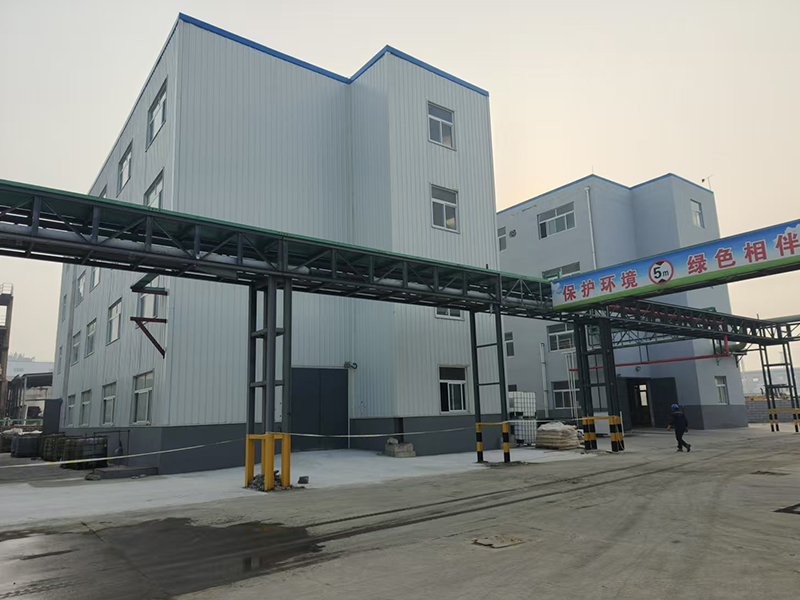
Our manufacturing facilities are located in Jiangxi and Shandong provinces, serving as our primary production centers. The Jiangxi plant is a brand-new facility equipped with state-of-the-art production lines and advanced manufacturing technologies, while our Shandong plant provides robust production capacity with years of operational excellence. Operated by skilled manufacturing teams and adhering to strict quality management systems, our factories ensure efficient, stable, and scalable production that meets both domestic and international standards.
With automated DCS control systems, environmental closed-loop emission scrubbing, and over 50,000 metric tons of annual polymer and water-reducing agent capacity, LANZO delivers exceptional quality batch-to-batch repeatability for chemical formulators across the globe.
Explore our full line of specialized flocculants, water-purifying matrices, and performance additives developed for custom industrial chemical blending.
High-grade coagulant agent optimized for primary chemical precipitation, turbidity settling, and phosphorus removal in municipal and industrial effluents.
Advanced polycarboxylate superplasticizer formulation delivering exceptional fluidizing power and water reduction in dense slurry systems.
Medium-to-high charge cationic polymer designed specifically for biological sludge conditioning and organic wastewater clarification.
Ultra-high molecular weight anionic formulation built for rapid mining slurry clarification, metallurgical thickening, and coal washing.
High-basicity PAC compound providing exceptional hydrolytic destabilization and micro-floc formation across varying pH ranges.
Acid-resistant polymer matrix engineered for solid-liquid extraction in acidic leach systems and complex inorganic saline environments.
Dithiocarbamate polymer composite delivering non-reversible precipitation of nickel, copper, zinc, and mercury from plating wastewater.
High-efficiency water clarifier for offshore and onshore reinjection systems, rapidly eliminating oil-in-water carryover and solids.


